
How Paint Line Conveyor Architecture Dictates Finishing Line Performance
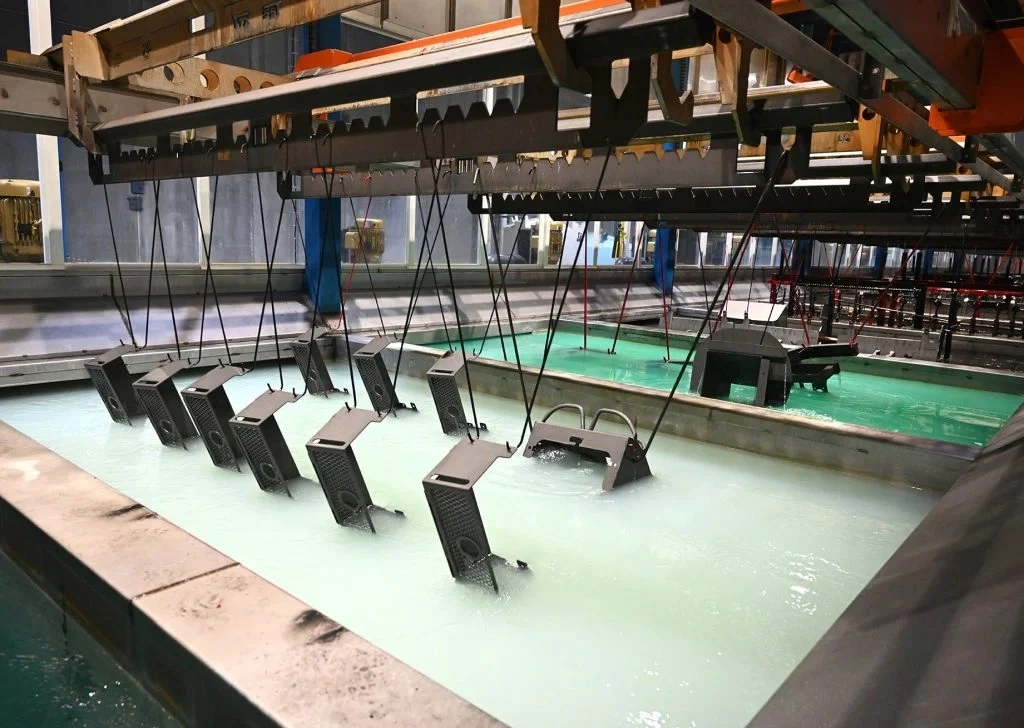
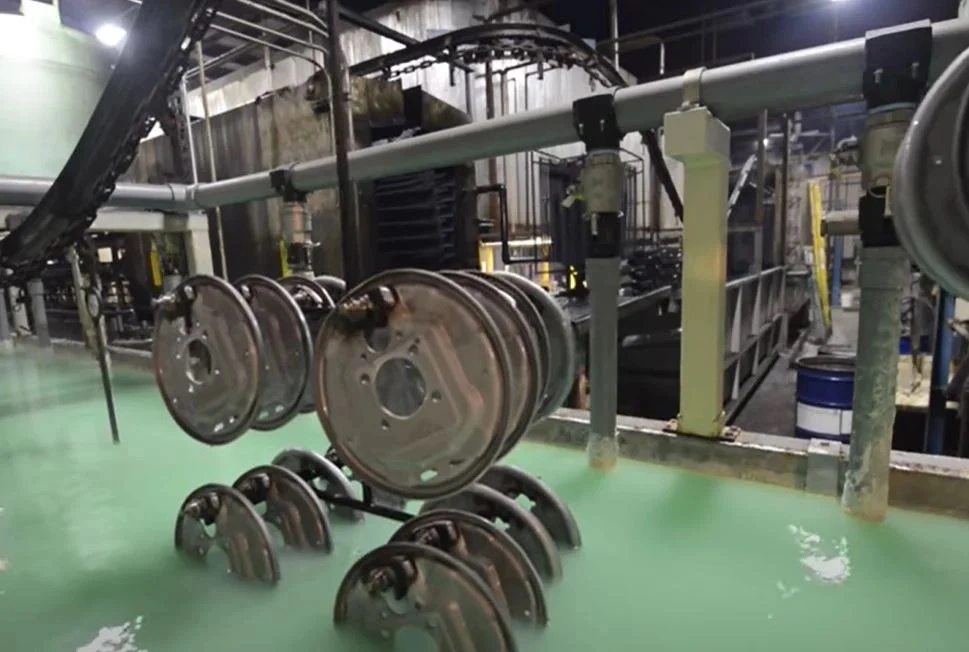
In automated finishing operations, the paint line conveyor serves as the central infrastructure that governs throughput, process consistency, and final coating quality. Unlike static manufacturing equipment, the conveying system interacts with every stage—pretreatment, spray application, flash-off zones, and curing ovens—making its design, material selection, and control logic pivotal to first-pass yield. A conveyor that fails to maintain precise indexing, uniform spacing, or stable thermal characteristics introduces variability that no spray booth or oven can fully compensate for. This article examines the engineering principles behind high-performance conveying systems, drawing on quantitative data from installations managed by HANNA across automotive, industrial equipment, and consumer goods manufacturing sectors. We analyze how conveyor architecture, material science, and control integration directly impact line efficiency, energy consumption, and defect rates.
1. Conveyor Topologies for Wet Paint and Powder Lines
The selection of a conveyor configuration must align with product geometry, coating chemistry (liquid vs. powder), and required production flexibility. Each topology imposes distinct constraints on line layout, maintenance protocols, and process control.
1.1 Overhead Monorail Systems
Overhead monorail conveyors represent the most widely deployed solution due to their simplicity and minimal floor space footprint. Parts suspend from trolleys traveling along a continuous I-beam track, driven by a friction or caterpillar chain. These systems are suitable for consistent part geometries and steady-state production. However, they introduce specific engineering challenges:
Thermal bridging: The continuous chain traverses through curing ovens, conducting heat outward and elevating energy consumption. In ovens operating at 180–220°C, chain temperatures can degrade lubricants and accelerate wear.
Lack of accumulation: Any downstream stoppage forces the entire line to halt, causing parts to remain in oven zones beyond specified dwell times—a primary source of over-cure defects.
Limited speed variation: The entire line operates at a single speed, preventing optimization of individual zones such as pretreatment dwell versus oven cure time.
1.2 Power-and-Free Overhead Systems
Power-and-free conveyors incorporate a secondary track that allows carriers to accumulate independently of the main propulsion chain. This design delivers critical advantages for complex finishing lines:
Zone isolation: Carriers can be stopped before spray booths for color change or quality inspection while upstream sections continue operation.
Independent speed profiling: Different segments—pretreatment, spray, flash-off, cure—can operate at optimal speeds. For example, the oven section can run slower to accommodate heavy castings while the spray booth maintains higher throughput.
Maintenance continuity: Sections can be taken offline for service without halting the entire production line.
These capabilities come with increased capital cost and control complexity, requiring sophisticated PLC programming to manage carrier routing, collision avoidance, and zone interlocking.
1.3 Inverted (Floor-Mounted) Conveyors
For large fabrications, automotive body-in-white, or parts with unstable hanging geometries, inverted conveyors provide a stable transport platform. The chain and carriers run in floor channels, with fixtures rising vertically to present parts at ergonomic heights. Engineering considerations include:
Contamination susceptibility: Floor-mounted chains are exposed to pretreatment chemicals, overspray, and debris, requiring robust sealing, stainless steel components, and automated wash-down systems.
Oven floor integration: The conveyor must withstand the same oven temperatures as the parts, necessitating heat-resistant rollers, expansion joints, and precise alignment to prevent buckling under thermal stress.
2. Thermal Management: Conveyor Influence on Oven Uniformity
The paint line conveyor is not a passive component in the curing process; its mass, spacing, and entry pattern actively shape oven temperature profiles. Three parameters demand rigorous engineering attention.
2.1 Carrier Mass and Heat Sink Loading
Each carrier absorbs thermal energy from the oven, acting as a heat sink that must be compensated by burner systems. Using finite element analysis (FEA), engineers calculate the specific heat absorption of carrier trains. In systems where carriers utilize lightweight aluminum alloys or stainless steel with open-web designs, oven energy consumption decreases by 12–18% compared to solid carbon steel carriers. Additionally, lighter carriers reduce drive motor loads and chain tension, extending mechanical component life.
2.2 Spacing Uniformity and Airflow Disturbance
Irregular part spacing creates turbulence and temperature gradients inside the oven. When a large gap occurs, oven PID controllers may overshoot, then undershoot as the next part enters—a phenomenon known as thermal shock. Automated spacing control using photo-eye arrays maintains consistent pitch (typically within ±150 mm variation), allowing oven airflow and burner modulation to stabilize. Field data from HANNA-engineered lines show that maintaining spacing uniformity reduces oven temperature deviation from ±8°C to ±3°C, directly correlating with a 40% reduction in cure-related rejects.
2.3 Chain Expansion and Contraction Cycles
Continuous chain conveyors experience thermal expansion as they exit the oven and contraction as they cool. Without proper take-up assemblies and expansion loops, this cycling causes chain elongation, sprocket misalignment, and eventual drive system failure. High-quality systems incorporate automatic tensioners with load cells that maintain constant chain tension across temperature ranges from ambient to 200°C.
3. Integration with Spray Booths: Grounding, Indexing, and Cleanliness
Whether applying liquid paint or powder coating, the conveyor must provide a reliable grounding path and precise positioning to achieve consistent film build.
3.1 Electrical Continuity for Electrostatic Application
Electrostatic spray processes require a continuous ground path from the part through the carrier to the conveyor rail. Any interruption—caused by coating build-up on hangers, worn trolley wheels, or grease contamination—leads to poor transfer efficiency, Faraday cage defects, and increased material consumption. Advanced conveyor systems integrate:
Automatic grounding verification: Resistance measurement between part and earth; alarms activate when resistance exceeds 1 megohm.
Self-cleaning trolley wheels: Carbon-fiber brushes or spring-loaded contacts that maintain conductivity despite coating accumulation.
Hanger stripping stations: In-line thermal or abrasive systems that remove accumulated coating from carriers without interrupting production.
3.2 Indexing Precision for Automated Applicators
Robotic spray cells and reciprocators rely on precise conveyor positioning. Any slippage, backlash, or speed variation results in inconsistent film thickness—particularly critical for automotive clearcoats and basecoats where tolerances are ±5 microns. Servo-driven indexing conveyors with absolute encoder feedback achieve positioning repeatability of ±1 mm, enabling consistent overlap patterns and edge coverage.
4. Predictive Maintenance and Lifecycle Cost Optimization
The total cost of ownership for conveying systems extends far beyond initial procurement. Three domains dominate operational expenditure:
Lubrication strategy: Overhead conveyors require precise lubrication intervals. Automated lubrication systems that apply high-temperature synthetic grease (rated for 250°C) to chain pins and trolley wheels extend chain life by 3–5 years compared to manual greasing, which often leads to under- or over-lubrication. In a recent HANNA installation, automated lubrication reduced annual lubricant consumption by 40% while increasing chain replacement intervals from 4 years to 7 years.
Wear component monitoring: Chain links, wear strips, and sprockets must be replaced at optimized intervals. Conveyors with modular chain designs allow section replacements without disassembling the entire system, reducing downtime by 70% for wear-related repairs.
Drive energy consumption: Friction losses dominate energy use. Using low-friction polymer wear strips instead of steel-on-steel contact reduces drive motor load by 15–20%. For a line operating 6,000 hours annually, this translates to 50,000–80,000 kWh savings.
5. Application-Specific Conveyor Engineering
5.1 Automotive Assembly Lines
Automotive finishing demands high throughput (up to 60 jobs/hour) with full traceability. Conveyor specifications include:
Load capacities up to 1,200 kg per carrier for body-in-white.
RFID tagging for part tracking and recipe management across primer, basecoat, and clearcoat zones.
Cleanroom-compatible materials for critical topcoat applications.
Skewed carrier designs to present parts at optimal angles for robotic spray.
5.2 Heavy Equipment and Agricultural Machinery
Large fabrications—some exceeding 5 meters in length and 3,000 kg—require specialized conveying solutions:
Wide carrier spacing (minimum 3 meters) to prevent part-to-part contact during rotation.
Powered rotating hooks or turntables within spray booths to allow complete coverage without manual repositioning.
Reinforced overhead structures with redundant load paths to ensure safety in high-bay ovens.
5.3 Appliance and General Finishing
High-volume consumer goods lines prioritize color-change flexibility and compact footprints:
Compact power-and-free systems with vertical storage loops for buffer capacity without expanding floor space.
Quick-change hanger designs to accommodate varying product families with minimal tooling changeover.
Modular conveyor sections that can be reconfigured as product mix evolves.
6. Smart Conveyor Systems: Data Integration and Process Control
Modern paint line conveyor platforms function as data acquisition hubs. Embedded sensors provide:
Real-time position tracking: Carrier location data synchronizes spray gun triggers, oven zone burners, and pretreatment spray nozzles to within milliseconds.
Load cell monitoring: Detects jams or overload conditions before they cause mechanical failure or product damage.
Vibration analysis: Accelerometers on drive units and major sprockets enable predictive maintenance by identifying bearing wear or chain misalignment before catastrophic failure.
Energy profiling: Sub-metering of conveyor drives correlates energy consumption with production volume, identifying opportunities for idle reduction and speed optimization.
When integrated with a plant-wide SCADA or MES system, this data enables statistical process control that links conveyor performance metrics to final coating quality. For instance, a trend of increasing drive motor current may indicate rising friction due to lubrication degradation or contaminant build-up, allowing intervention during scheduled downtime rather than unplanned stoppage.
Frequently Asked Questions (FAQ)
Q1: How do I determine whether a monorail or power-and-free conveyor is appropriate for my paint line?
A1: The decision hinges on three factors: accumulation requirements, speed variability needs, and maintenance flexibility. Monorail systems suffice for single-product lines operating at constant speed with minimal downtime tolerance. Power-and-free is indicated when you need to: (a) isolate zones for color changes or quality holds without stopping the entire line, (b) run different sections at varying speeds (e.g., slower oven dwell for heavy parts while maintaining booth throughput), or (c) perform maintenance on sections without total production stoppage. Calculate the cost of downtime per hour; for operations exceeding $3,000/hour in lost revenue, power-and-free typically delivers payback within 18–24 months.
Q2: What are the most common conveyor-related defects in liquid paint lines?
A2: The primary defects are: (1) dirt and contamination from flaking carrier coatings or degraded chain lubricant, (2) inconsistent film build due to grounding failures or indexing inaccuracies, (3) thermal distortion from uneven oven spacing causing localized under- or over-cure, and (4) physical damage from part-to-part contact during accumulation or transfer. Regular audits of carrier cleanliness, ground continuity, and spacing consistency reduce these risks. Implementing a scheduled hanger stripping process—thermal or chemical removal of accumulated coating—prevents contamination before it affects production.
Q3: How does conveyor speed fluctuation affect oven cure profiles for wet paint?
A3: Liquid paint cure cycles are highly sensitive to both temperature and time. Conveyor speed variation alters dwell time in each oven zone. If the conveyor slows unexpectedly, solvents may flash off too rapidly, causing blistering; if it accelerates, solvents may remain trapped, resulting in solvent pop. High-quality systems use closed-loop speed control with encoder feedback to maintain setpoint within ±2%. Additionally, oven controllers should receive conveyor speed signals to dynamically adjust zone temperatures—a feature known as speed-compensated temperature control—which maintains consistent substrate temperature regardless of minor speed variations.
Q4: What maintenance intervals should be established for overhead paint line conveyors?
A4: For a two-shift operation (16 hours/day), recommended intervals are: daily visual inspection of chain tension and lubrication levels; weekly ground continuity verification on carriers; monthly cleaning of photo-eyes and proximity sensors; quarterly inspection of wear strips and sprocket alignment; semi-annual chain elongation measurement (replacement recommended when elongation exceeds 3%); and annual thermal imaging of drive units to detect developing bearing failures. Automatic lubricators with programmable cycles should be serviced every 6 months. Facilities following this schedule typically achieve 15+ years of reliable operation from high-quality conveyor systems.
Q5: Can existing paint line conveyors be retrofitted with smart monitoring technology?
A5: Yes, retrofitting is both feasible and cost-effective. Add-on systems include: vibration sensors on drive units and major sprockets; current transducers on motor drives; photo-eye arrays for spacing monitoring; and RFID gate readers for carrier tracking. These sensors feed into a PLC or edge gateway with cellular connectivity for remote alerts. Typical retrofits cost 15–25% of a new conveyor system and achieve payback through reduced unplanned downtime within 12–18 months. HANNA has completed such retrofits across multiple facilities, documenting average downtime reductions of 35% and maintenance cost savings of 25%.
The paint line conveyor represents far more than a material transport mechanism—it is the foundational infrastructure upon which finishing line performance is built. By applying rigorous engineering to conveyor architecture, thermal management, grounding integrity, and predictive maintenance, manufacturers achieve higher first-pass yields, lower energy costs, and greater production flexibility. HANNA continues to partner with finishing operations worldwide to design, upgrade, and optimize these critical systems, ensuring that the conveyor becomes a competitive advantage rather than a process constraint.
Related News
Learn More + -
How Paint Line Conveyor Architecture Dictates Finishing Line Performance
In automated finishing operations, the paint line conveyor serves as the central infrastructure that governs throughput, process consistency, and fin ...View Details2026-11-06 -
Paint Line Conveyor Systems Excellence: 9 Critical Parameters for Precision Coating & Operational Longevity
In industrial powder coating operations, the conveyor system is far more than a material handling asset—it functions as the central nervous system th ...View Details2026-11-06 -
7 Critical Factors When Selecting a Paint Line Conveyor for Industrial Finishing
A Paint line conveyor is the backbone of any automated coating operation. It determines throughput, coating consistency, and uptime. A poorly specif ...View Details2026-11-06 -
Optimizing Paint Line Conveyor Systems for Zero-Defect Powder Coating: A Technical Guide
Powder coating operations demand absolute precision in material handling. The paint line conveyor systems form the central nervous system of any hig ...View Details2026-11-06 -
Paint Line Conveyor Systems: A Technical Guide for Powder Coating Engineers
A deep technical guide to paint line conveyor selection, design, maintenance, and throughput for powder coating operations. Built for engineers and pl ...View Details2026-11-06 -
Paint Line Conveyor Systems: How to Choose the Right Design
The performance of a powder coating line rarely depends on the spray guns alone. What really decides coating consistency, throughput, and reject rate ...View Details2026-11-06